Guide to an Overview of Equipment in a Motorcycle Manufacturing Plant
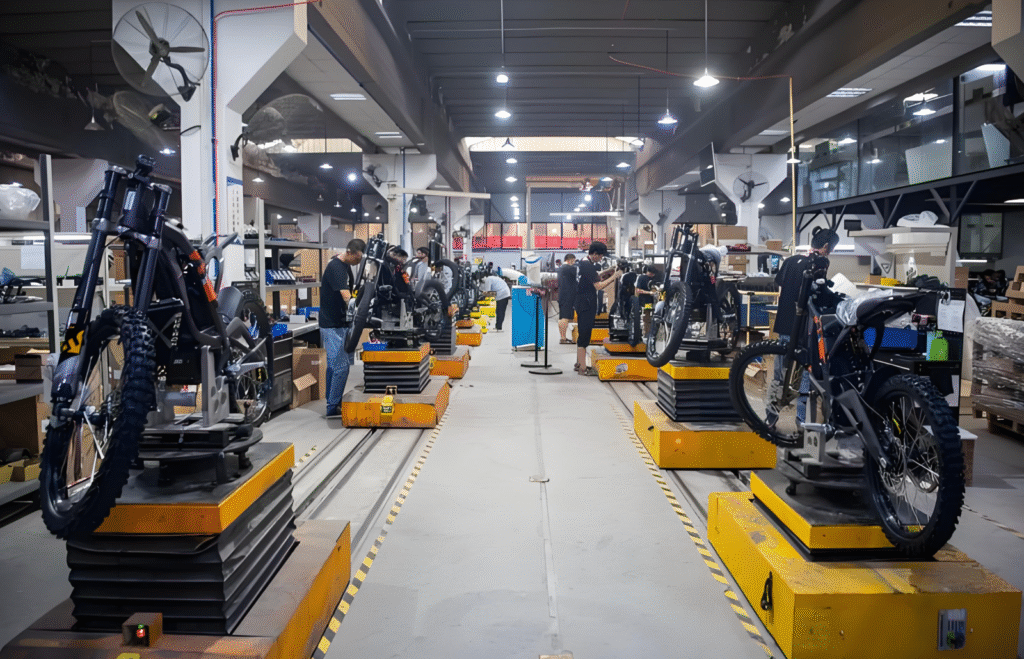
A motorcycle plant integrates machining, fabrication, painting and assembly. Engine blocks/heads are milled, bored and honed on 5-axis CNC centers, then die-cast and heat-treated. Tube frames are laser-cut, CNC-bent and welded by robots before e-coat primer and 180 °C bake. Final assembly uses pallet conveyors, servo tire mounters and vacuum brake fillers, achieving 90–120 s takt. Chassis dynos, emission benches and rain chambers validate power, Euro 5 limits and leak-tightness. RFID pallets, AGVs and Andon systems drive paperless traceability and 95 % first-run yield.
Below is a complete detailed motorcycle-plant equipment list, organized by manufacturing flow.
1. Engine Machining Area
1.1 Cylinder Block / Head Line
Equipment
Core Function
Typical Configuration & Process Details
Horizontal Machining Center (HMC)
Multi-face machining in one clamping
12 000 r/min spindle, BT50 taper, 24-tool chain magazine; rough/finish milling and boring of deck face, crank bore, cam bore.
Vertical Machining Center (VMC)
End faces, angled holes, dowel holes
3- or 5-axis, automatic part flip station; finish milling of combustion chambers and ports on cylinder head.
Gun-drilling Machine
Deep oil holes
Gun drill Ø4–Ø8 mm, L/D up to 20; 7 MPa high-pressure internal coolant.
CLD NOx, NDIR CO/HC, CVS dilution; Euro 5 compliant.
Rain Test Chamber
Leak tightness
Nozzle pitch 600 mm, 10–15 mm/min rainfall, 30 min duration; floor turntable included.
6. Logistics & IT
Equipment
Core Function
Typical Configuration & Process Details
Automated Warehouse (AS/RS)
Machined blanks & parts storage
Stacker 18 m high, 2000 locations, double-deep forks; WMS real-time sync with ERP.
AGV (SLAM Navigation)
Inter-station material flow
1 t payload, ±10 mm SLAM accuracy; auto-charge and call-button integration.
Andon System
Line-side escalation
3-color tower lamp + 55″ display, trigger ≤5 s.
7. Quick Reference Table
Phase
Key Equipment
Typical Parameter / Process KPI
Engine Machining
HMC, honing, gun-drill
Ra ≤ 0.4 µm; bore tolerance H6
Frame Fab
Tube bender, welding robot
Tube thinning ≤10 %; weld penetration ≥2 mm
Paint
Pretreat, e-coat, bake
Salt spray ≥720 h; film 20–30 µm
Assembly
Pallet line, tire mounter, filler
Takt 90–120 s/unit; first-run yield ≥95 %
Testing
Dyno, emissions, rain
Speed accuracy ±0.1 km/h; 30 min rain no leak
When building a motorcycle plant anywhere on the globe, treat “climate risk” as a design input that cascades through the entire chain—building envelope, equipment, logistics and people. Below are practical notes for four representative climate zones.
Tropical Monsoon / Hot-humid (South China, SE Asia)
Typhoon & Downpour – Structure: main hall rated for ≥40 m/s wind (50-year return); roof clips upgraded; drain pipes oversized +20 %. Outdoor gantry cranes have storm anchors. – Drainage: site level ≥ +0.5 m vs. municipal road; 500 mm flood barriers; duplex power pumps in underground sump.
Corrosion & Heat – Roof and wall panels: Al-Zn alloy + PVDF, 1000 h salt-fog rating. – Ventilation: local spot-cooling at engine test stands; roof exhaust fans ≥12 air changes/h.
Equipment Choice – Electrical enclosures ≥ IP54 with internal A/C at 28 °C; CNC coolant tanks dosed with biocide to stop summer mold.
Frost Protection – Double-skin insulated wall (K ≤ 0.45 W/m²·K); inflatable dock seals and heated air curtains on loading bays. – Compressed-air dryers rated at –40 °C dew point to prevent ice in valves.
Cold-Start Support – Engine cold-test benches use 40 °C pre-heat water loops. – Wet sprinkler system replaced by dry or pre-action type.
Low Pressure – Boilers and burners derated to 0.8 atm; drying ovens retuned for altitude. – Generator room fitted with boost fans and voltage regulators to offset >15 % power loss at 3 500 m.
UV & Dust – Wall cladding with UV-resistant film; rooftop fans have sand-proof louvers. – Compressor intake filters with 50 % larger dust-holding capacity.
Human Safety – Office areas use on-site oxygen-enrichment (23 % O₂) to cut altitude sickness incidents.
Temperate Continental / Four-season (North China, US Midwest)
Large Diurnal/Seasonal Swings – Floor slabs designed with temperature joints (-20 °C to +40 °C). – Roof clerestory vents open in summer for free cooling, closed in winter for insulation.
Energy Strategy – Winter: reclaim 60 °C coolant from engine dyno for space heating—cuts gas use ~15 %. – Summer: switch to ground-source heat pumps for cooling, reducing chiller load.
Universal Playbook
Build a “climate-risk-mitigation” matrix: classify typhoon, torrential rain, blizzard, sandstorm and extreme temperature as Tier-1 risks with dedicated SOPs.
Modular critical equipment: A/C units, cooling towers and compressor stations built as containerized skids that can be crane-lifted to safety within 72 h.
Closed-loop operations: MES continuously logs ambient data (T, RH, wind, pressure) and triggers automatic protective actions to eliminate sudden shutdowns.
By combining a regional climate database, modular design and dynamic O&M, a motorcycle plant can be rapidly replicated, safely commissioned and reliably operated in any climate zone on earth.
This two-wheel electric motorcycle / scooter assembly process, aligned with top domestic manufacturers’ standards, follows a systematic workflow centered on the frame, adhering to “mechanics first, electronics second; inner parts first, outer parts later” principles. Starting with pre-assembly preparation (material sorting, tool calibration), it proceeds through 10 core stages: chassis pre-assembly, motor/transmission fitting, suspension installation,…
الأنواع المعلقة تنقل الحمل من الأرض إلى السقف، فتتطلب سقفًا بقدرة ≥2.5 ك ن/م²، معوّقات اهتزاز وتسوية دورية، توفر أرضية خالية لغرف نظيفة أو مرور رافعات، لكنها ترفع الكلفة ١٥–٢٥٪. الأرضية تُثبَّت بأرض ٥٠٠ كغ/م²، تتحمل أحمالًا أكبر، تسويتها بسيطة وصيانتها من سطح الأرض، لكنها تشغل مساحة وتترك ثقوبًا عند النقل. اختر التعليق فقط إذا…
Electric forklift production follows three pillars: modular pre-assembly, online control of torque, sealing and electronics, and full-load bench validation. A typical line runs 28 U-shaped stations at 5-6 min takt, fed by three sub-lines for mast, battery and axle, uses AGV shuttles, servo presses and RFID racks, and stores every torque and test value in…
The buried plate chain conveyor line is a key equipment for universal automobile assembly, featuring a robust structure with drive/tensioning units, heavy-duty chains, anti-skid platform plates and an intelligent electric control system. It offers adjustable speed (2-6m/min), high load capacity (2T per workstation) and stable, low-noise operation. Its underground design saves floor space, and it…
Assembly-line strapping machines are grouped by automation, frame style, material and direction; choices range from side-seal and sword types for pallets to press types for fluffy bales. PET cord delivers steel-like strength at lower weight. Match speed and tension to carton size and line takt; servo length cuts strap use 5-8 %. Low-table or horizontal…
Automobile factories rely on eight main types of assembly conveyors to ensure efficient and orderly production, each tailored to specific operational needs. Overhead and chain slat conveyors handle medium-heavy to heavy loads, ideal for body transfer and heavy assembly transportation. Floor slat and skid conveyors offer high positioning accuracy, supporting precision processes like chassis and…